 Custom parts
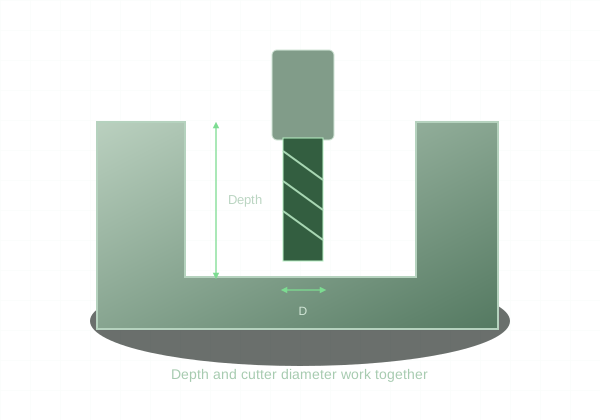
Increase stiffness where possible. A tighter tolerance does not prevent a flexible part from moving during machining.
Deflection changes the cut
Cutting and clamping forces can bend thin features. When the force is removed, the material springs back, leaving a different geometry from the one present under load. Vibration can also affect surface finish. Wall height and unsupported span matter as much as nominal thickness.
Material removal can release stress
Stock can contain residual stress. Removing material asymmetrically may cause a part to move as it becomes thinner. Broad plates with deep pockets and thin bottoms are particularly sensitive. A final flatness requirement therefore needs to be evaluated with the complete geometry and stock condition.
Design stiffness into the geometry
Shorten unsupported walls, add ribs where they do not obstruct function, and use generous transitions. Keep enough material for stable clamping. Where possible, avoid a tall thin wall with a tight dimension that must be produced after most supporting stock is removed.
Plastics add more variables
Engineering plastics are generally less stiff than metals and more sensitive to temperature. Clamp pressure and measurement force can change apparent dimensions. There is no universal minimum wall thickness across aluminum, steel, acetal, and UHMW; select the feature proportions around the actual material and use.